At Katalyst Engineering Services, we continually strive to drive innovation by deftly utilizing these resources, changing the issues encountered by various industries and fields with potential solutions.
At Katalyst Engineering Services, we continually strive to drive innovation by deftly utilizing these resources, changing the issues encountered by various industries and fields with potential solutions.

To improve manufacturing performance with AI, you need to integrate machine learning, computer vision, and digital twins into production, maintenance, and planning workflows. Artificial intelligence in manufacturing is no longer a futuristic concept. It’s a practical tool that factories use today to cut downtime, boost quality, and make faster operational decisions.
For engineering teams exploring manufacturing services that combine AI with hands-on plant-floor expertise, the opportunity is clear: move from isolated pilots to scalable, engineered AI systems.
AI in manufacturing engineering is the use of machine learning, computer vision, optimization, generative AI and related techniques to analyze manufacturing data and support decisions across production, maintenance, quality, engineering and supply-chain workflows.
To define AI in manufacturing engineering, you need to describe systems that learn from operational data, predict outcomes, and optimize processes without explicit programming for every scenario.
AI in manufacturing engineering refers to the application of machine learning, computer vision, natural language processing, and advanced analytics to improve manufacturing operations, from production planning to equipment maintenance and product design validation.
Unlike traditional automation, AI systems adapt to changing conditions, identify patterns humans might miss, and continuously improve performance over time.
To build effective AI systems in factories, you need AI engineers who understand both data science and industrial operations.
An ai engineer in manufacturing typically –
Artificial intelligence engineering in manufacturing is less about coding in isolation and more about embedding intelligence into physical production systems.
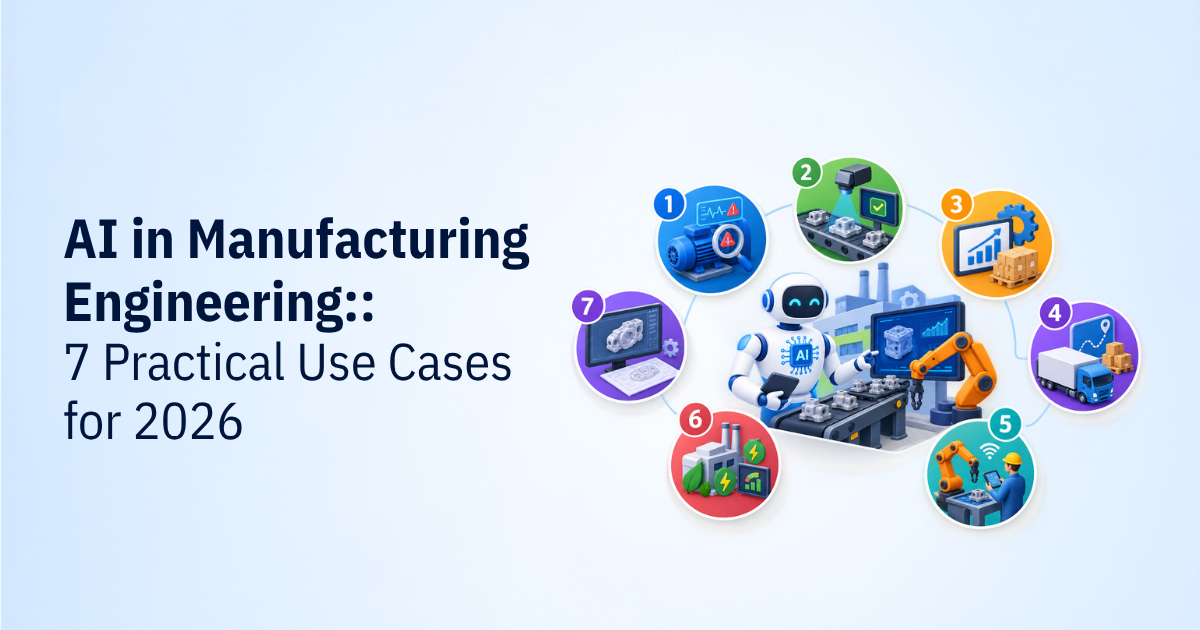
To achieve quick wins with AI, you need to focus on high-impact use cases like predictive maintenance, quality inspection, and production optimization.
1. Predictive Maintenance
AI analyzes sensor data to predict equipment failures before they happen, reducing unplanned downtime by up to 50%.
2. AI-Powered Quality Inspection
Computer vision systems detect defects in real time, cutting scrap rates and improving consistency.
3. Production Planning Optimization
AI models balance demand, inventory & capacity to reduce bottlenecks and improve throughput.
4. Intelligent Robotics
AI-enabled robots adapt to variable environments and support human-machine collaboration.
5. Digital Twins
Virtual models simulate production changes before implementation, reducing risk and accelerating innovation.
6. Generative AI for Engineering
AI assistants generate work instructions, summarize maintenance history, and flag design issues.
7. Supply Chain Optimization
AI forecasts demand, optimizes inventory, and improves logistics resilience.
To create an AI factory, you need to combine IoT sensors, analytics platforms, machine learning models, and digital twins into a connected ecosystem.
| Component | Function |
| IoT Sensors | Collect real-time machine and process data |
| AI Analytics Platforms | Identify trends and anomalies |
| Machine Learning Models | Predict failures and optimize schedules |
| Digital Twins | Simulate changes before implementation |
| Computer Vision | Monitor quality and detect defects |
| Connected Engineering Systems | Enable seamless data flow across teams |
This integrated approach supports digital transformation in engineering initiatives that are scalable and sustainable.
To understand AI’s advantage, you need to compare it with traditional automation across key dimensions.
| Dimension | Traditional Automation | AI-Driven Manufacturing |
| Flexibility | Low (fixed workflows) | High (adapts to changes) |
| Maintenance | Reactive (fix after failure) | Predictive (fix before failure) |
| Quality Control | Manual or rule-based | Real-time computer vision |
| Implementation | High upfront cost, rigid | Modular, scalable, ROI-focused |
| Decision-Making | Human-dependent | Data-driven, automated insights |
Manufacturing AI should be introduced in stages. Start with a measurable production problem, validate the available data, test the solution in a controlled environment, and integrate it into plant workflows only after the pilot meets predefined criteria.
Phase 1: Identify the engineering problem
Define baseline KPI, failure mode, bottleneck or quality issue.
Phase 2: Validate data availability
Check sensors, historian, MES, maintenance records, images, labels and data quality.
Phase 3: Select the appropriate AI approach
Determine whether the problem requires ML, computer vision, optimization, anomaly detection, GenAI, simulation or conventional automation.
Phase 4: Build a controlled PoC
Use representative production data and define success criteria before development.
Phase 5: Validate in the production environment
Test accuracy, latency, false positives, false negatives, reliability and operational impact.
Phase 6: Integrate with plant systems
Connect the solution to MES, ERP, SCADA, CMMS, PLC/edge systems or other relevant infrastructure.
Phase 7: Deploy with human oversight
Define who receives alerts, who approves actions and how exceptions are handled.
Phase 8: Monitor and scale
Track KPI improvement, model drift, system reliability and operational adoption.
For deeper insights on reducing bottlenecks with AI, see how AI-driven process mining is transforming production workflows.
To avoid pitfalls, you need to address data quality, legacy infrastructure, workforce readiness, and cybersecurity early.
To stay competitive, you need to prepare for autonomous production, generative AI assistants, and real-time sustainability optimization.
Explore how advanced robotics in manufacturing is enabling smarter, more flexible production.
Key Takeaways
The shift to AI in manufacturing engineering is already underway, with factories using predictive maintenance, computer vision, and digital twins to improve quality, efficiency, and competitiveness. Organizations that adopt engineered AI solutions today will be better positioned to navigate future market demands and accelerate innovation.
Planning an AI pilot for your manufacturing operation? Talk to Katalyst Engineering about identifying the right use case, data requirements and integration path.
1. What is AI in manufacturing engineering?
AI in manufacturing engineering uses machine learning, computer vision, and analytics to optimize production, maintenance, and design workflows.
2. How does an ai engineer contribute to manufacturing?
An ai engineer develops models for predictive maintenance, quality inspection, and production optimization while integrating AI with MES and ERP systems.
3. What are the top AI use cases in factories?
Predictive maintenance, quality inspection, production planning, robotics, digital twins, generative AI & supply chain optimization.
4. How long does it take to implement AI in manufacturing?
A manufacturing AI pilot can take several months, but timelines vary significantly based on data availability, integration complexity, validation requirements, production environment and use case. A well-scoped pilot should begin with predefined technical and business success criteria.
5. Is AI only for large manufacturers?
No. Small and mid-sized factories can start with targeted AI solutions like predictive maintenance or quality inspection.
6. What is a digital twin in manufacturing?
A manufacturing digital twin is a digital representation of a physical asset, process or system that is connected to relevant data and models so engineers can monitor, analyze, simulate, predict, or optimize its behavior. The degree of synchronization and real-time capability depends on the use case and architecture.
7. How does AI improve manufacturing quality?
AI-powered computer vision detects defects in real time, reducing scrap and improving consistency.
8. What are the main challenges of AI adoption in manufacturing?
Data quality, legacy infrastructure, workforce training, and cybersecurity.

Senior Vice President, Katalyst Engineering
Bhavik Shah is the Vice President of Global Engineering and Manufacturing at Katalyst Engineering, with over 22 years of experience in the engineering industry. He specializes in product development, R&D, and engineering delivery operations, driving innovative, design-led solutions across automotive, industrial, and off-highway sectors. Bhavik plays a key role in strengthening engineering strategies, building global partnerships, and delivering high-performance outcomes for clients.